Sheet Metal Enclosure Prototype
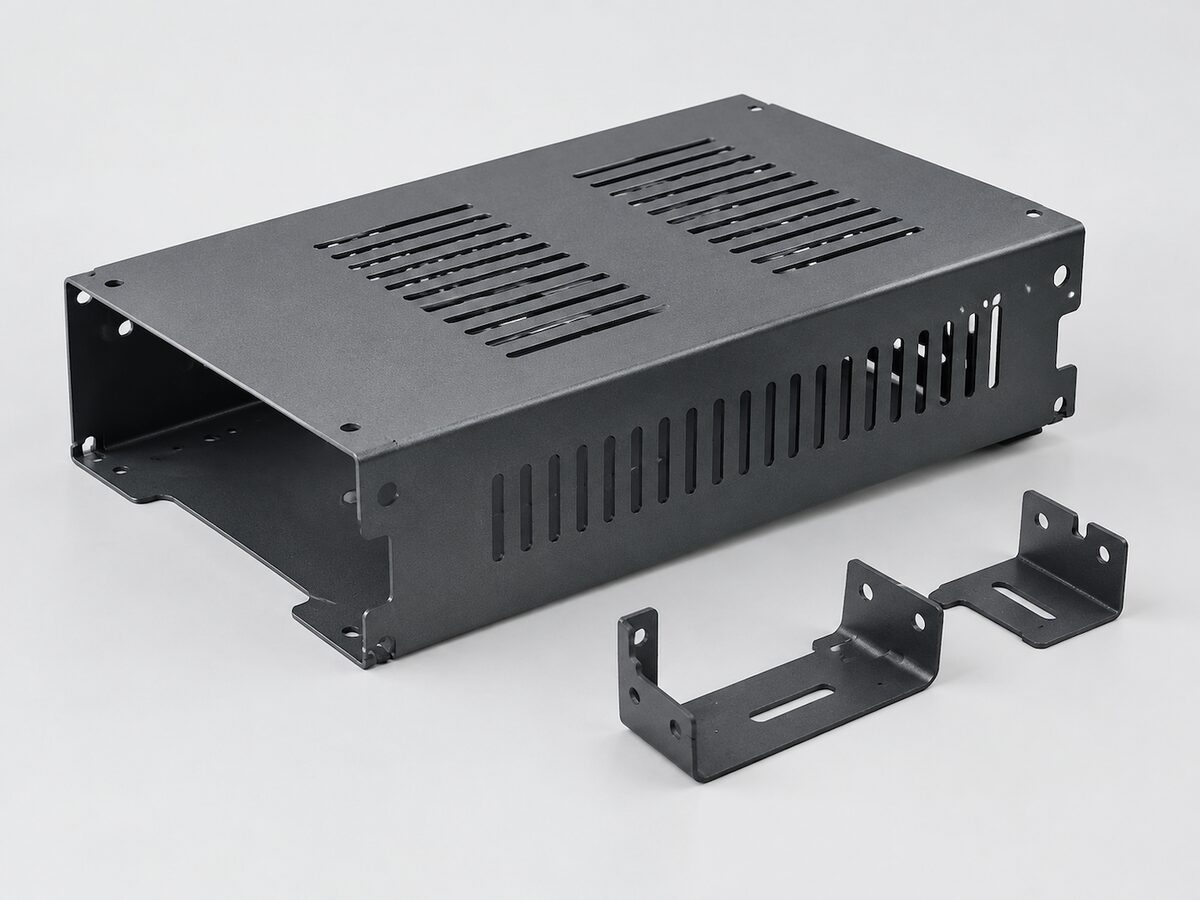
A prototype enclosure has to do three things at once: hold the electronics, look like the product and survive the assembly line. Sheet metal gets you there faster than a moulded housing when the design is still moving.
Where the tolerance actually goes
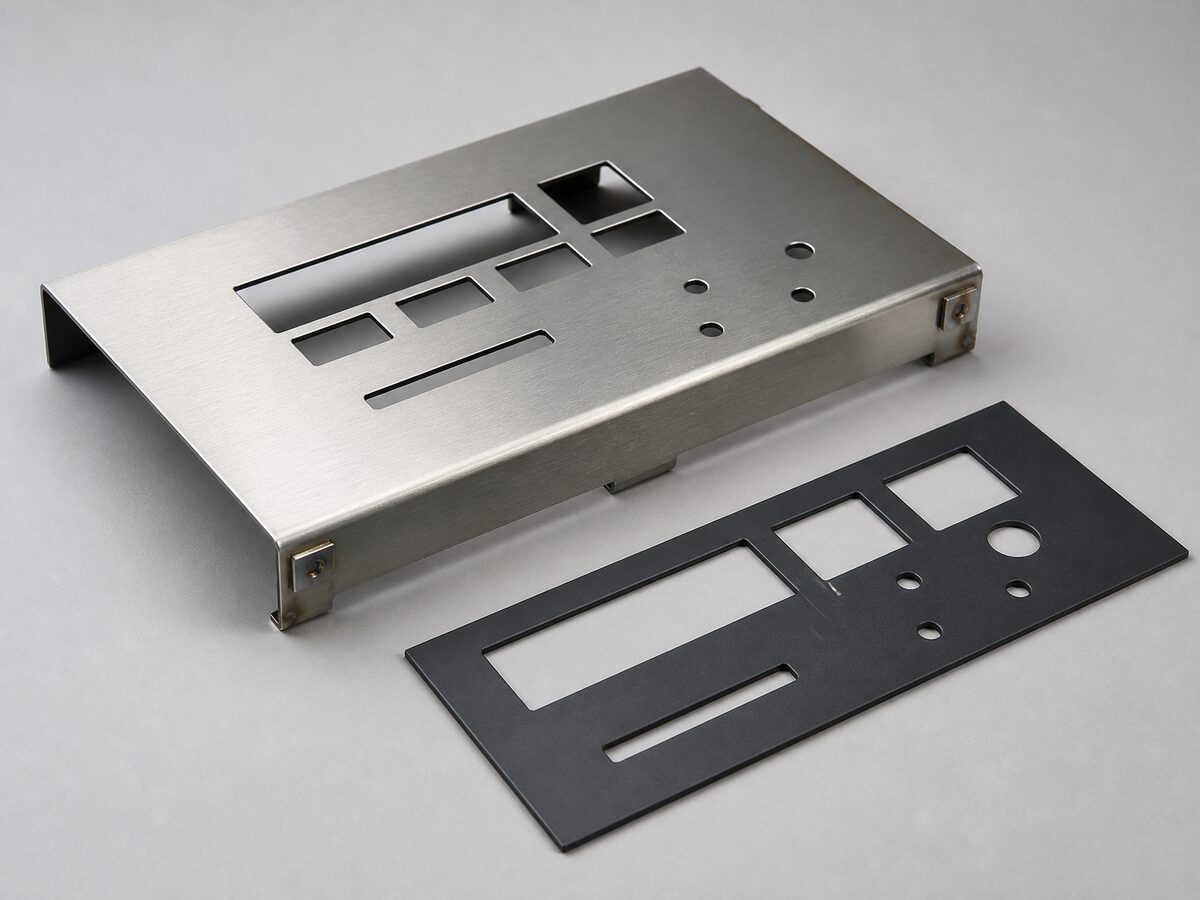
Laser cutting holds +/-0.1 mm on hole position. The bend sequence is where error accumulates, so we set the tooling against your drawing and check the first part on a granite table before running the batch.
For a 10 to 200 unit run we laser cut, form, weld if needed, install PEM hardware, then powder coat. Coating thickness adds 60 to 90 microns per face – if a dimension is critical after paint, tell us and we will compensate.
| Feature | Capability |
|---|---|
| Laser cut hole position | +/-0.1 mm |
| Formed feature position | +/-0.1 mm |
| Sheet thickness range | 0.5-6 mm (fibre laser), to 12 mm waterjet |
| Materials | Mild steel, stainless 304/316, aluminium, galvanised |
| Finishing | Powder coat, anodise, zinc plate, brushed |
| Lead time, 10-200 units | 5-8 working days |
Questions buyers ask
Do you need a 3D model or will a flat DXF do?
A folded STEP is best because it proves the bend sequence. A flat DXF works if you also send the bend lines and the material thickness.
Can you install threaded inserts and standoffs?
Yes – PEM nuts, standoffs and clinch studs are fitted before coating, so they stay flush.
What about silk screen or laser marking?
We can mark after coating, or leave it to your assembly line. Marking on a curved or coated surface is worth agreeing on a sample first.
More on materials and finishing on the sheet metal page. Upload a STEP or DXF on the quote form.